
The production process in a manufacturing unit is highly complicated, as it needs a proper movement of materials. Manufacturers have to deal with heavy materials, components, and manufacturing kits. That is why they use material handling equipment to ensure smooth workflow, reduced production times, and low downtime. However, while dealing with material handling systems, you can find them in two categories- On-floor and overhead models. To have higher productivity and keep your workers safe, you have to invest in the right material handling equipment. Now, we will help you to know how these on-floor movers differ from the overhead versions.
1.On-floor material handling equipment-
Most of the on-floor movers, like hydraulic pallet trucks, are affordable solutions, and they need minimal maintenance. Moreover, they can move the load along any unfixed path. For instance, you may use gravity conveyors to move a bulk amount of materials of consistent shapes.
BOPT, stackers, forklifts, and other trucks need a large amount of factory floor space to move your materials. Conversely, overhead cranes and other similar material handling systems do not need this floor space.
The capabilities of carrying load are higher than that of hand trucks due to weight constraints. Moreover, on-floor movers can result in safety risks for your equipment and workers. For instance, when you have loaded a forklift improperly, it may get turned over. Thus, this overturned forklift may injure your employees and damage your materials. Furthermore, they can leave a chance of human errors, and unbalanced loads may fall from the system, causing a mess. Conveyors, one of the on-floor movers, perform their operations at a human height and may injure workers at any time.
The installation process of conveyors is another hassle to users. When you have a big manufacturing facility managing a high volume of materials, conveyors may affect the traffic flow on the floor. To say simply, the floor space will become crowded due to the use of these on-floor movers.
2.Overhead systems to move materials
We have already been told that overhead material movers do not need much space to install and operate. Your workers can move freely in your manufacturing facility. Although some hoists and cranes need some floor-mounted systems, they have a very limited footprint in the floor space. What’s more, overhead lifting systems ensure the ultimate safety of workers and materials. You may also reduce the physical labour needed for material management and lifting solutions. Aerospace, automotive, and construction industries mostly use these overhead systems.
Let us have a look at the overhead mover used in different industries.
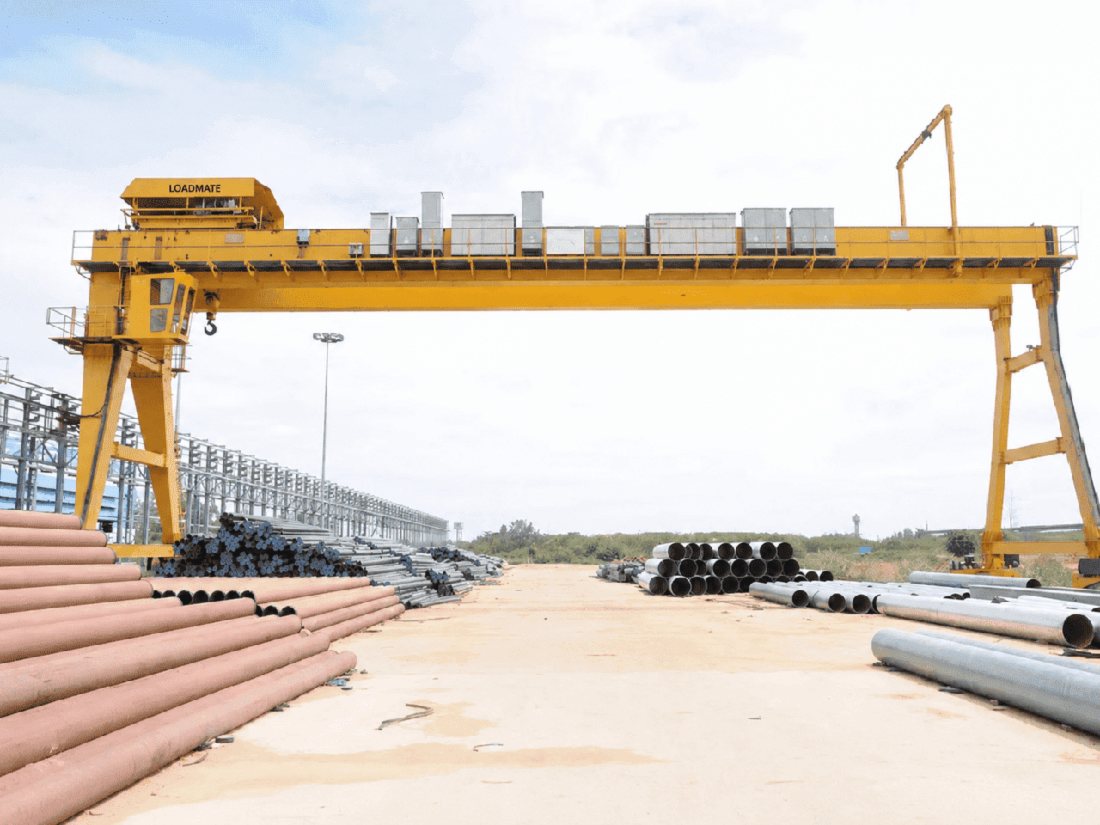
- Overhead cranes- These systems use hoists, hooks, and magnets to lift loads and move them. Gantry cranes, as one of the overhead systems, provide us with versatile solutions as they move on 3 axes. One is horizontal, and two of them are perpendicular. They can rotate in more than one direction.
- Monorails- Monorails perform their operation on tracks directly fitted to the roofing system of your manufacturing facility. However, they have some similarities to on-floor movers, as you can find restrictions to movements. Monorails are also the right choice to move your loads repeatedly over a path. You may prefer monorails to reach the risky and hard-to-access sites. As the overhead monorail puts the moving loads out of range of your workers, it may reduce the injury risk.
- Hoists- When you are looking for versatile systems to lift the suspended loads, you can choose these hoists. Hoists include a rope, wire, and chain to lift your loads, and they may have electrical, pneumatically, or manual operations.
To decide on the overhead lifting system, you have to focus on your manufacturing process and some other relevant factors.
3.Some common on-floor movers
- Hand trucks: These hand trucks are two-wheeled carts to move heavy objects manually. They have a vertical structure with integrated handles at the top section. Moreover, their bottom section includes a metal blade. The overall setup tilts backwards until it attains a proper balance. Dollies and carts are some common hand trucks used in different industries.
- Conveyors: You can find the application of conveyors in shopping malls, airports, and supermarkets. They can move heavy materials and small plates very quickly. Conveyors remain stable in one position with ancillary tools and add-ons to connect to the non-conveyor system. There are also portable conveyors useful in the logistics industry.
- Forklifts: These are small industrial systems with a forked platform, which needs power. The platform remains fitted to the front side that you can raise and lower easily to insert it to the place under your cargo. Modern forklifts need electric batteries for their operation. One of the major components of forklifts is the truck frame that creates the base part of the system. Other parts of a forklift are wheels, mast, and a counterweight.
Now, you can easily decide on on-floor and overhead material handling systems. From the comparative analysis, we have found that overhead cranes are a better and safer choice for manufacturers and other workers in your industry. Based on your purpose and needs, you can invest in the right material handling equipment and increase your productivity.
4.EOT Cranes vs Forklifts
Pros of E.O.T. Cranes
- Longevity: These cranes are the Methuselahs of material handling, boasting life expectancies exceeding 25 years. Custom-built to fit your specific needs, they are less prone to damage.
- Safety Maximization: Essentially becoming a part of your facility’s infrastructure, E.O.T. cranes offer a unique design that navigates around obstacles, thereby reducing the risk of accidents.
- Herculean Capacity: With a minimum load capacity of 1 ton and a maximum reaching 550 tons, these cranes can out-lift any forklift or other crane types on the market.
- Spatial Efficiency: An E.O.T. crane operates above your workspace, negating the need for floor-level navigation and optimising your floor layout for other uses.
Cons of E.O.T. Cranes
- High Initial Investment: Although they offer greater long-term value, the upfront cost of E.O.T. cranes can deter some businesses.
- Limited Portability: Being integrated into your facility's structure makes relocating the E.O.T. cranes a cumbersome, if not impossible, task.
- Storage Height Constraints: The height of your storage racking system may need to be compromised to accommodate the crane’s dimensions.
Pros of Forklifts
- Mobility: Being relatively smaller and self-propelled, forklifts can be driven through narrow aisles and even transferred between facilities if needed.
- Lower Upfront Costs: The initial financial outlay for a forklift is generally less imposing, making it a go-to option for businesses operating on a tighter budget.
Cons of Forklifts
- Shorter Lifespan: With a typical life expectancy ranging from 10 to 15 years, forklifts wear out significantly faster than E.O.T. cranes.
- Labour-Intensive: Operating a forklift often involves multiple personnel and is generally more labour-intensive, which can add up in terms of operational costs.